- sales@bjbod.com
- Mon - Sat at 7:00AM to 9:00PM
Inquiry
Form loading...
What Is the Best China Metalworking Parts Supplier? The answer depends on your drawings, materials, tolerances, production volume, and quality expectations. A suitable partner should do more than offer a low quotation. It should explain manufacturing risks before production begins.
In Metalworking Of Parts, practical experience matters. A reliable supplier can discuss CNC machining, stamping, turning, milling, forging, surface treatment, and inspection with specific examples. Ask how workers control a 0.02 mm tolerance, protect finished surfaces, and record inspection results. Request material certificates, first-article reports, and photographs from the production line. Small details reveal a lot. Does the supplier check tool wear? Does it label batches clearly? Can it explain what happens when a dimension fails?
Dr. W. Edwards Deming, a respected manufacturing and quality expert, said, “Quality comes not from inspection, but from the improvement of the production process.” That principle remains useful when comparing Chinese suppliers. Inspection catches defects, but stable processes prevent repeated defects. Look for documented procedures, calibrated measuring equipment, traceable materials, and responsive engineering communication. Certifications can support trust, but they cannot replace evidence.
No supplier is perfect. Neither is every drawing. A thoughtful buyer should leave room for clarification, testing, and honest revision. The best partner may not be the cheapest or the most polished online. It is the supplier that understands your part, proves its capability, communicates clearly, and improves when something goes wrong. That is where confidence begins.
What Is the Best China Metalworking Parts Supplier?
A reliable metalworking parts supplier defines quality with evidence, not attractive claims. ISO 9001 provides a structured quality management system. It requires controlled procedures, documented inspections, corrective actions, and traceable records. Ask how the supplier handles drawing revisions, nonconforming parts, and operator training.
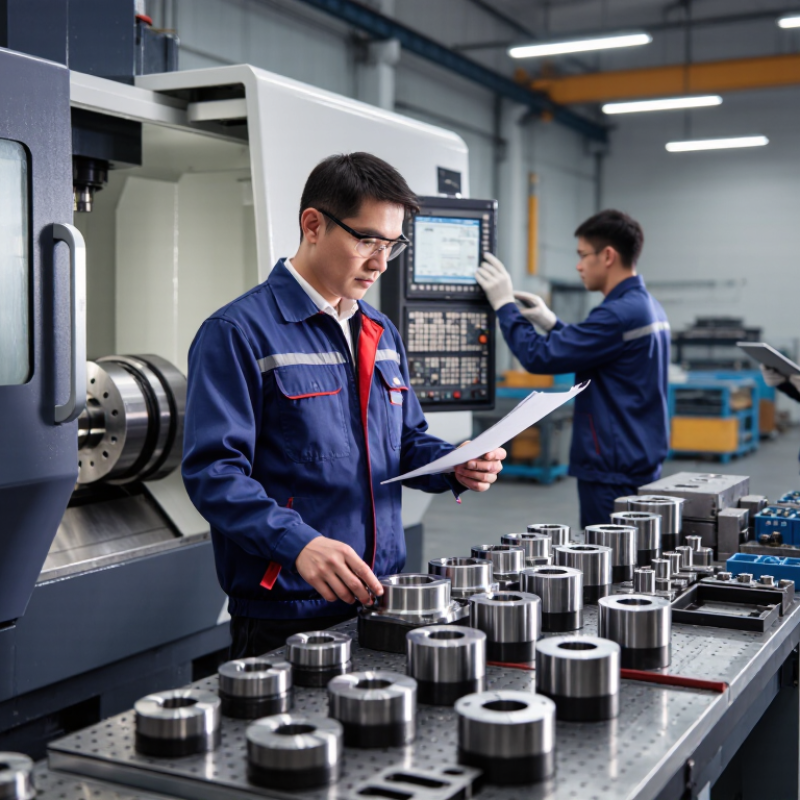
ISO 2768 can clarify general tolerances when individual dimensions lack specific requirements. However, it does not replace engineering judgment. A drawing requiring ±0.05 mm needs tighter process control than ordinary fabrication. The supplier should confirm equipment capability before production begins. Calibrated micrometers, gauges, and coordinate measuring machines can verify critical features. Inspection reports should identify the measured dimension, actual result, instrument, and inspector.
Details matter.
Experienced suppliers review tolerances during quotation, not after machining. They may recommend datum adjustments, tool compensation, or a first-article inspection. Material certificates and batch identification also support reliable traceability. Still, no quality system is perfect. A clean report cannot correct poor fixture design or unclear drawings. Suppliers should openly discuss risks and document corrective actions. That honesty is more useful than promising zero defects. Before placing a larger order, request sample parts, process records, and evidence that ±0.05 mm dimensions remain stable across the full batch.
| Quality Dimension | Relevant Standard or Reference | Practical Requirement | Evidence to Request | Quality Indicator |
|---|---|---|---|---|
| Quality management system | ISO 9001:2015 | The supplier should operate a documented quality management system covering relevant production sites, processes, and product scope. | A current certificate issued by an accredited certification body, including the legal entity, site address, certification scope, issue date, expiry date, and certificate status. | Verify scope and validity |
| Drawing and specification control | ISO 9001:2015, documented information controls | The supplier should control drawing revisions, customer specifications, approved changes, and obsolete documents before production begins. | Revision-controlled drawings, order review records, engineering change logs, and approval records for deviations or substitutions. | Revision traceability required |
| General dimensional tolerances | ISO 2768-1 | If individual tolerances are not specified on a drawing, the drawing must state the applicable ISO 2768 tolerance class, such as fine, medium, coarse, or very coarse. | A drawing showing the selected tolerance class and inspection results demonstrating conformity with the applicable limit values. | Class must appear on drawing |
| General geometrical tolerances | ISO 2768-2 | Where applicable, the drawing should identify the geometrical tolerance class for features without individually stated geometrical tolerances. | Datum structure, geometric inspection reports, and measurement results for straightness, flatness, perpendicularity, symmetry, or run-out as specified. | Use only when specified |
| Tight dimensional tolerance | Customer drawing and inspection plan | A tolerance of ±0.05 mm must be stated explicitly on the drawing or purchase specification. It should not be assumed solely from ISO 2768. | First-article inspection report, calibrated measurement records, process capability data where appropriate, and a control plan for critical dimensions. | Drawing-specific requirement |
| Measurement capability | ISO 9001 measurement-resource controls; ISO 10012 as a measurement-management reference | Inspection equipment must be suitable for the required accuracy. A ±0.05 mm requirement generally needs controlled, calibrated equipment and a defined measurement method. | Calibration certificates, equipment identification, measurement resolution, environmental controls where relevant, and measurement-system evaluation records. | Calibration must be traceable |
| Material conformity | Purchase specification and applicable material standard | Material grade, condition, hardness, coating, or heat-treatment requirements must match the approved drawing and purchase order. | Material certificates, heat-treatment records, coating reports, batch or heat numbers, and traceability from raw material to finished part. | Batch traceability required |
| Process control | ISO 9001:2015 operational planning and control | Critical machining, forming, welding, finishing, or assembly steps should have defined parameters, acceptance criteria, and reaction plans. | Process flow diagrams, control plans, setup sheets, work instructions, in-process inspection records, and nonconformance procedures. | Controls should match risk |
| First-article approval | Customer-specific approval process | Before full production, the supplier should verify dimensions, material, surface treatment, functionality, and special characteristics on a representative sample. | First-article inspection report linked to the drawing revision, sample identification, measurement method, and approval status. | Approve before mass production |
| Final inspection and release | ISO 9001:2015 release of products and services | Finished parts should be released only after planned inspections and tests are completed and accepted. | Final inspection reports, sampling plan, lot identification, quantity verification, packaging inspection, and authorized release records. | Release records required |
| Nonconforming product control | ISO 9001:2015 control of nonconforming outputs | Nonconforming parts must be identified, segregated or controlled, dispositioned, and prevented from unintended shipment. | Nonconformance reports, corrective-action records, concession approvals, rework instructions, and customer notification records when applicable. | Containment and CAPA required |
| Supplier and subcontractor control | ISO 9001:2015 externally provided processes | Outsourced heat treatment, plating, coating, grinding, or testing should be controlled under defined technical and quality requirements. | Approved subcontractor list, purchase specifications, subcontractor certificates, incoming verification records, and performance reviews. | Subcontracted steps need control |
| Packaging and shipment protection | Customer packaging specification | Parts should be protected against corrosion, impact, contamination, mixing, and loss of traceability during transport and storage. | Packaging standard, labeling sample, corrosion-prevention method, quantity verification, and shipment inspection checklist. | Protect parts and identity |
| Continuous improvement | ISO 9001:2015 improvement requirements | The supplier should analyze defects, customer complaints, process trends, and corrective-action effectiveness rather than relying only on final inspection. | Corrective-action reports, root-cause analysis, trend charts, internal audit results, management-review outputs, and improvement records. | Evidence-based improvement |